This CNC plastic turning services guide explains material selection, tolerance risks, machining constraints, and RFQ details for precision nylon, POM, PTFE, PEEK, acrylic, and other turned plastic parts.
What Are CNC Plastic Turning Services?
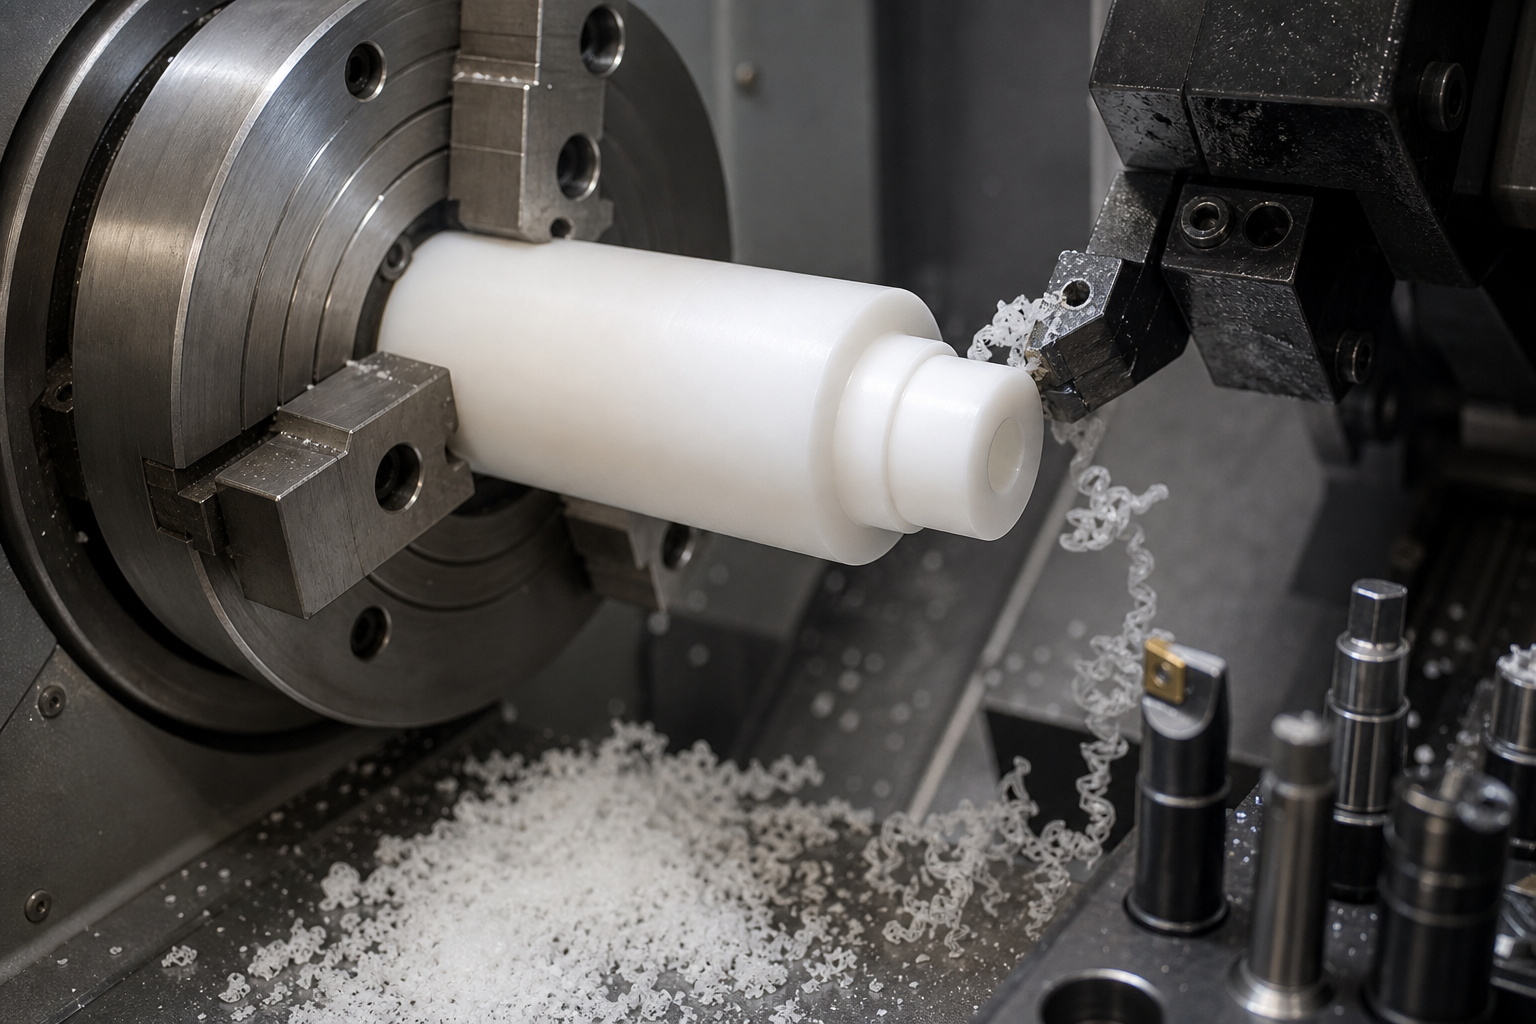
CNC plastic turning services produce cylindrical and rotational plastic parts such as bushings, spacers, rollers, sleeves, threaded components, seals, knobs and custom machine parts. The process uses CNC lathes, turning centers or Swiss-type machines to cut plastic stock into precision components.
Plastic turning is not the same as metal turning. Plastics can be softer, more elastic, more heat-sensitive and more dimensionally sensitive. A capable supplier must understand both machining and polymer behavior.
CNC Plastic Turning Materials at a Glance
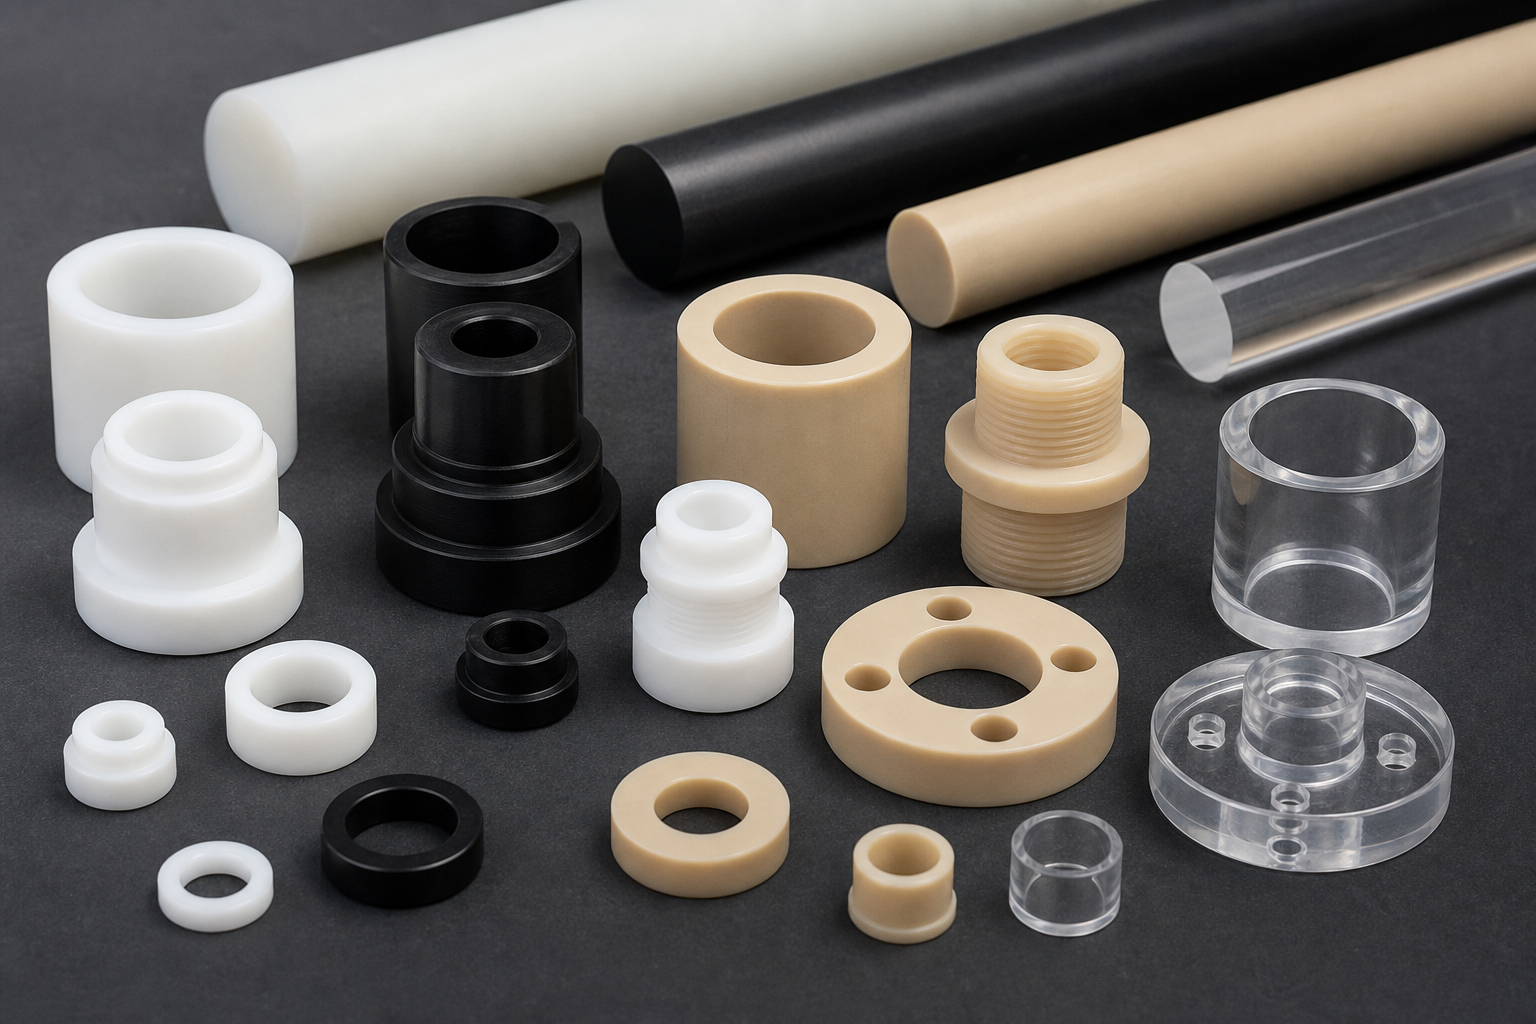
| Materiaal | Common turned parts | Main machining concern |
|---|---|---|
| Nylon PA6/PA66 | Bushings, rollers, wear parts | Moisture absorption and dimensional movement |
| POM/acetal | Sleeves, gears, low-friction parts | Thermal expansion and sharp edge control |
| PTFE | Seals and low-friction parts | Soft material and clamping deformation |
| PEEK | High-performance components | Cost, tool control and heat management |
| Acrylic/PMMA | Clear knobs and optical parts | Chipping and cracking |
| UHMW-PE | Rollers and wear components | Flexibility and workholding stability |
For nylon stock, review the nylon CNC machining guide alongside the grade, moisture condition and drawing.
When CNC Turning Is Better Than Molding
CNC turning is often better for low-volume, high-mix or tight-detail round parts. It avoids mold cost and allows fast dimensional changes. It is also useful when the material is difficult to mold or when the part needs post-machined precision features.
Injection molding may be better for high-volume production, complex non-round shapes and low unit cost after tooling.
Compare the tooling, quantity and design-change considerations in the CNC machining versus injection molding guide before fixing the production route.
Tolerance Challenges in Plastic Turning
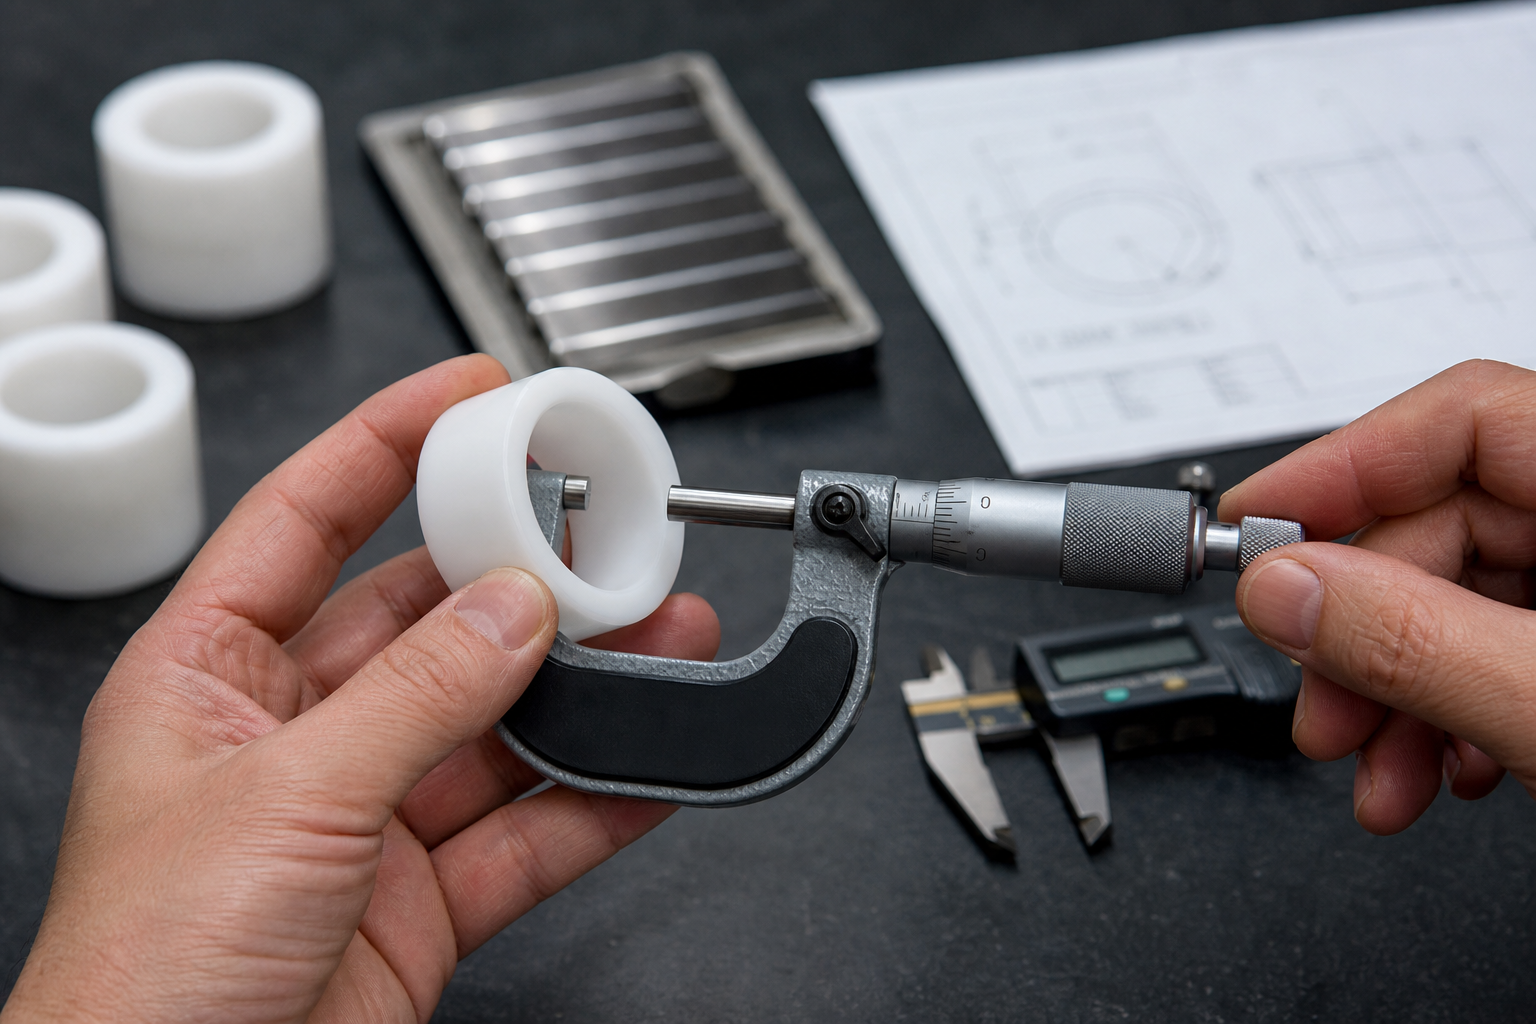
Plastic parts can expand, relax or deform more than metal parts. A tolerance that looks simple in aluminum or steel may be difficult in nylon or PTFE.
Important tolerance factors include:
- Thermische uitzetting during machining and inspection.
- Moisture absorption for nylon.
- Clamping pressure and part deformation.
- Internal stress in extruded or cast stock.
- Thin-wall deflection.
- Surface finish requirements.
Common CNC Plastic Turning Problems
| Probleem | Waarschijnlijke oorzaak | Oplossing |
|---|---|---|
| Oval or distorted parts | Clamping pressure or thin wall | Use softer jaws, support tooling and realistic wall design |
| Slechte oppervlakteafwerking | Wrong tool geometry or heat | Adjust tool, feed, speed and coolant/air blast |
| Afwijking in afmetingen | Material movement or heat | Control temperature and inspection timing |
| Burrs or fuzzy edges | Soft plastic or dull tool | Use sharp tools and proper deburring |
| Cracking in acrylic | Stress or aggressive cutting | Reduce cutting stress and use suitable tooling |
Design Tips for Turned Plastic Parts
Use generous radii where possible, avoid extremely thin walls, define only critical tolerances tightly and keep noncritical dimensions realistic. For threaded plastic parts, confirm thread depth, mating material and assembly torque.
For press-fit parts, account for creep and relaxation. For long slender parts, ask whether custom fixturing or a different process is needed.
CNC Turning Quote Review: Fit, Heat and Material Movement
| Part Feature | Typical Plastic Risk | What the RFQ Should Define |
|---|---|---|
| Long slender shaft or tube | Deflection, chatter, taper or runout after release | Support, datum, length-to-diameter ratio, runout and inspection method |
| Thread or sealing land | Fit changes with moisture, temperature, burrs or creep | Thread standard, mating part, torque, clearance, surface and service state |
| Thin wall or flange | Clamping distortion or loss of roundness | Workholding, free-state condition, wall support and measurement sequence |
| Wear or sliding surface | Material is selected by name without load, speed or counterface data | Load, speed, temperature, lubrication, mating material and life target |
CNC plastic turning is not simply metal turning with a slower feed. Nylon, PTFE, PEEK, POM and UHMW respond differently to heat, clamping, moisture, chip evacuation and stress relief. A reliable quote states the material grade, stock condition, tolerance basis, inspection state, finish and quantity instead of hiding those assumptions in a unit price.
Gerelateerde lezen
Veelgestelde vragen
What plastics can be CNC turned?
Common choices include nylon, POM, PTFE, PEEK, acrylic, UHMW-PE, HDPE and PC. The best material depends on load, temperature, friction, chemicals and dimensional requirements.
Are CNC turned plastic tolerances the same as metal tolerances?
Not automatically. Thermal expansion, moisture absorption, clamping deformation, stress relief, geometry and inspection temperature must be included in the tolerance decision.
When is CNC turning better than injection molding?
Turning is often better for round prototypes, low volumes, quick design changes and some difficult-to-mold materials. Molding usually becomes more economical after volume and geometry stabilize.
What should I send for a CNC plastic turning quote?
Send the drawing and CAD, exact material or performance target, quantity, tolerance notes, finish, service conditions, mating parts, inspection reports and packaging requirements.
Can turned plastic parts be supplied with inspection reports?
Yes, when the RFQ defines the report level. Specify critical dimensions, datums, material traceability, first-article or sampling requirements, measurement method and packaging identification.
Request a CNC Plastic Turning Review
For CNC plastic turning services, send the drawing and mating-component details for bushings, sleeves, shafts, rollers or other round parts. Nylon Plastic can review the material, stock form, workholding and functional fits before quotation.
Wat moet er worden opgenomen en overeengekomen voordat er een offerte wordt opgesteld?
- Include CAD and drawing revision, exact grade or approved alternative, color, quantity by phase, annual demand, destination and timing.
- Identify bores, runout and coaxiality datums, threads, sealing lands, mating parts and acceptable workholding marks; state inspection temperature and free-state or assembled measurement.
- Provide service load, speed, lubrication, temperature, humidity and chemicals where relevant; define insert installation, deburring, finishing, first-article records and packaging.
Nylon Plastic can machine nylon, POM, PTFE, PEEK, acrylic and other engineering plastics for prototypes and production components.
Nylon Plastic connects CNC machining with modified material selection and production inspection. For unfilled PA, PA-GF20 and PA-CF30, the quote should distinguish machined stock from injection-molded pellets and account for fiber orientation, tool wear, moisture and the final service condition.
Separate material, setup or fixtures, turning, secondary milling, inserts and inspection in the quote. Agree the sample fit and inspection method with the mating part; machined PA stock and injection-molding pellets are different purchase forms.

