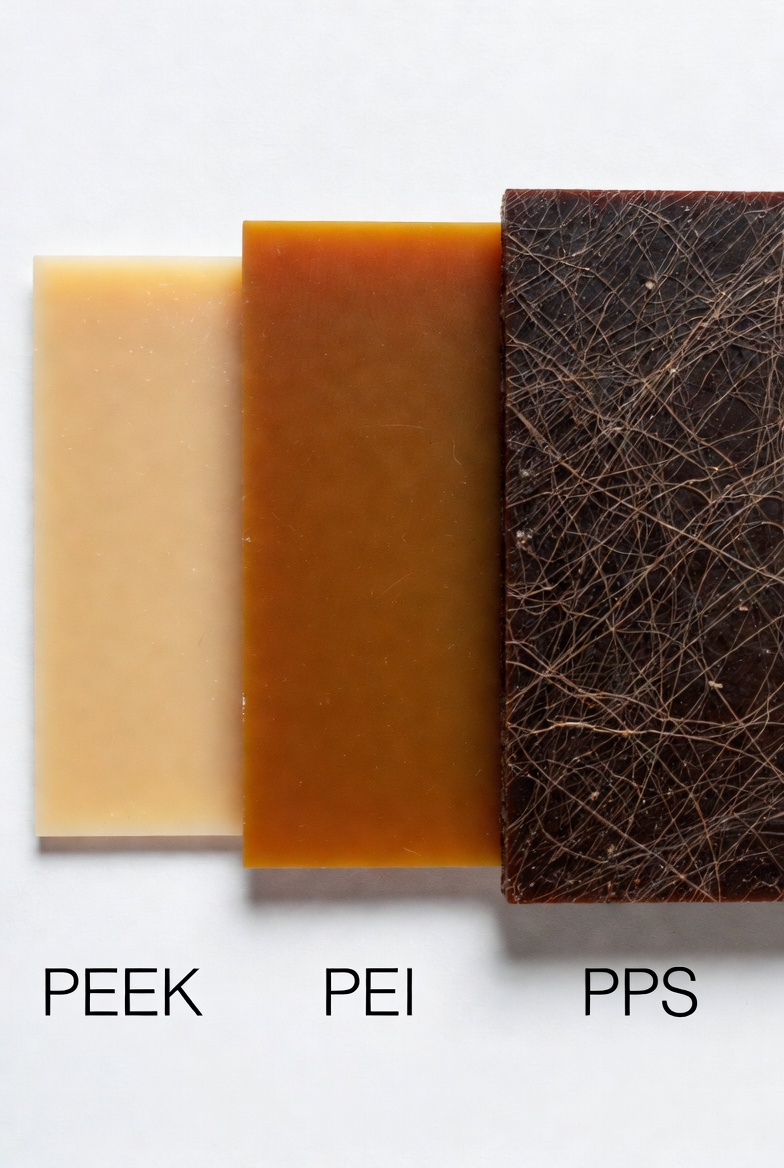
High-temperature engineering plastics are selected when a part must retain useful strength, insulation, chemical resistance or dimensional stability after exposure to heat. PEEK, PEI, PPS, PPA and LCP can all be suitable, but they solve different problems. The best choice depends on the actual temperature profile, load, chemical exposure, geometry, process route, volume and documentation requirement.
A datasheet maximum is not the same as a safe design temperature. Ask whether the part is loaded continuously, exposed to short thermal peaks, cycled through heat and humidity, or required to meet a flame or dielectric standard at a defined wall thickness. A material review should also identify whether injection molding, CNC machining or another route can produce the required geometry and inspection condition.
Start with the service condition
| Vereiste | Wat moet worden gedefinieerd | Why it changes the selection |
|---|---|---|
| Temperatuur | Continuous temperature, peak temperature, dwell time and thermal cycling | Heat deflection and short-term melt or glass-transition data do not describe the same condition |
| Mechanische belasting | Static load, impact, vibration, creep and load direction | Reinforcement and fiber orientation can matter more than nominal tensile strength |
| Milieu | Water, steam, fuel, cleaners, acids, bases, solvents and oxygen exposure | Chemical resistance can change with temperature, stress and exposure time |
| Compliance | Flame, smoke, dielectric, medical, food or customer-specific requirements | The exact grade, color and wall thickness may control the approval |
Material selection at a glance
| Materiaalfamilie | Usually considered for | Main strengths | Belangrijkste risico’s |
|---|---|---|---|
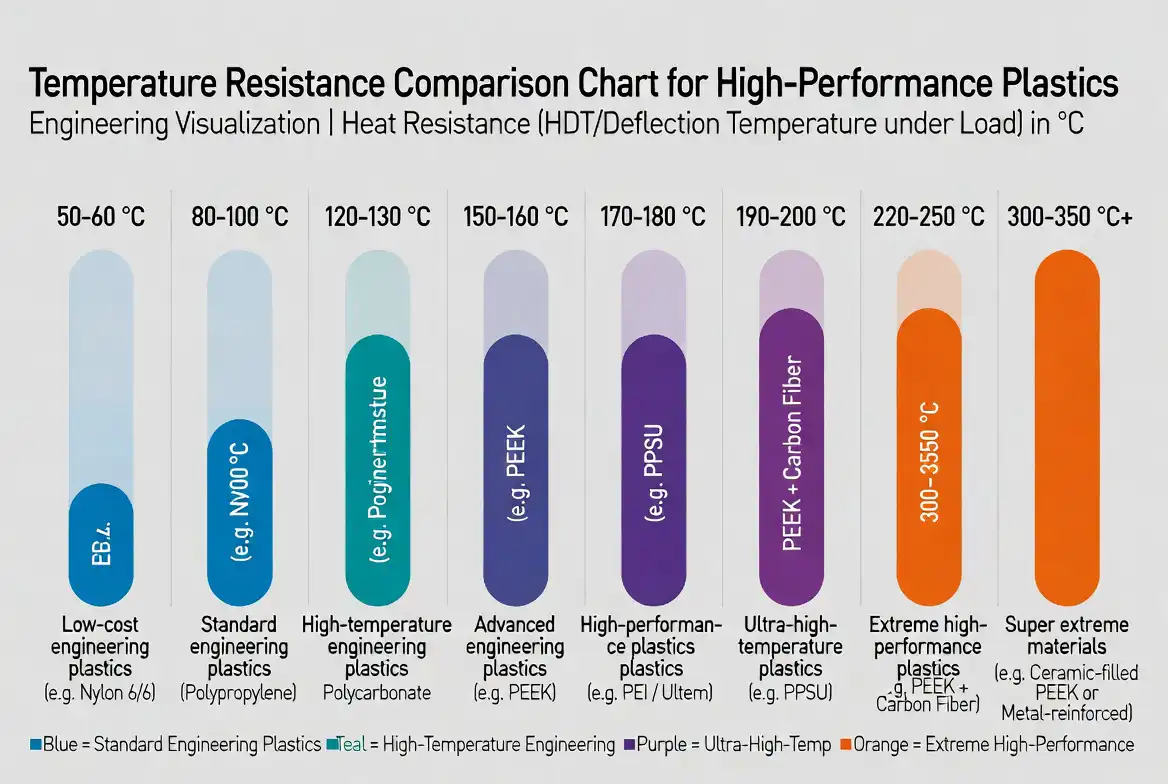
| PEEK | Severe heat, chemicals, wear and sterilization | High temperature capability, chemical resistance, fatigue and wear performance | High resin and processing cost; demanding drying, tooling and molding control |
| PEI / Ultem | Electrical parts, fixtures, housings and heat-resistant molded parts | Amorphous processing, dielectric stability, flame performance in suitable grades | Stress cracking with some chemicals; moisture and grade-specific drying requirements |
| PPS | Chemical process parts, automotive under-hood components and electrical parts | Low moisture uptake, chemical resistance and dimensional stability | Unfilled grades can be brittle; reinforced grades are directional and abrasive to tools |
| PPA | Cost-sensitive high-temperature structural and automotive parts | Useful stiffness and heat performance at lower cost than PEEK | Moisture, hydrolysis, grade variation and long-term creep require validation |
| LCP | Thin-wall connectors, fine features and high-speed electrical components | Very good flow, low shrinkage and high-temperature electrical performance | Anisotropy, weld-line strength and gate orientation can dominate the design |
These are selection directions, not universal property guarantees. The exact grade, reinforcement, color, wall thickness and conditioning state should appear in the RFQ. For PEEK parts made by CNC machining, see the PEEK CNC machining guide. For PEI grade and process decisions, see the PEI Ultem material guide.
When PEEK, PEI, PPS, PPA or LCP is the better fit
Choose PEEK when the combination of heat, chemical exposure, wear and mechanical duty leaves little margin. It is often justified for demanding valve seats, seals, bearings, pump components, high-temperature fixtures and selected medical or aerospace parts. The purchase decision should include the cost of drying, high-temperature processing, tool materials, machining and inspection. A less expensive polymer may be sufficient if the actual load and exposure are moderate.
Choose PEI when electrical, flame and dimensional performance are important at elevated temperature. PEI is often practical for connectors, coil forms, sensor housings, fixtures and molded components that need an amorphous high-performance polymer. Check the chemical environment carefully, especially ketones, chlorinated solvents and strong bases. The PEEK vs PEI comparison is useful when both families appear feasible.
Choose PPS when chemical exposure and moisture stability are more important than impact toughness. Glass-filled PPS can support stiff, dimensionally stable components in aggressive environments. Gate orientation, weld lines and brittle failure modes should be reviewed before final approval. Use representative parts when testing, because a flat material coupon cannot reproduce the same flow orientation or insert stress.
Choose PPA when the program needs a high-temperature engineering material but does not justify PEEK cost. PPA can work well for reinforced automotive and industrial parts, but its moisture and hydrolysis behavior must be matched to the application. Choose LCP when thin-wall flow, fine pitch, low shrinkage and electrical performance are the primary constraints. LCP is not simply a lower-cost substitute for PEEK or PEI; its value comes from its flow and precision behavior.
Processing and design risks
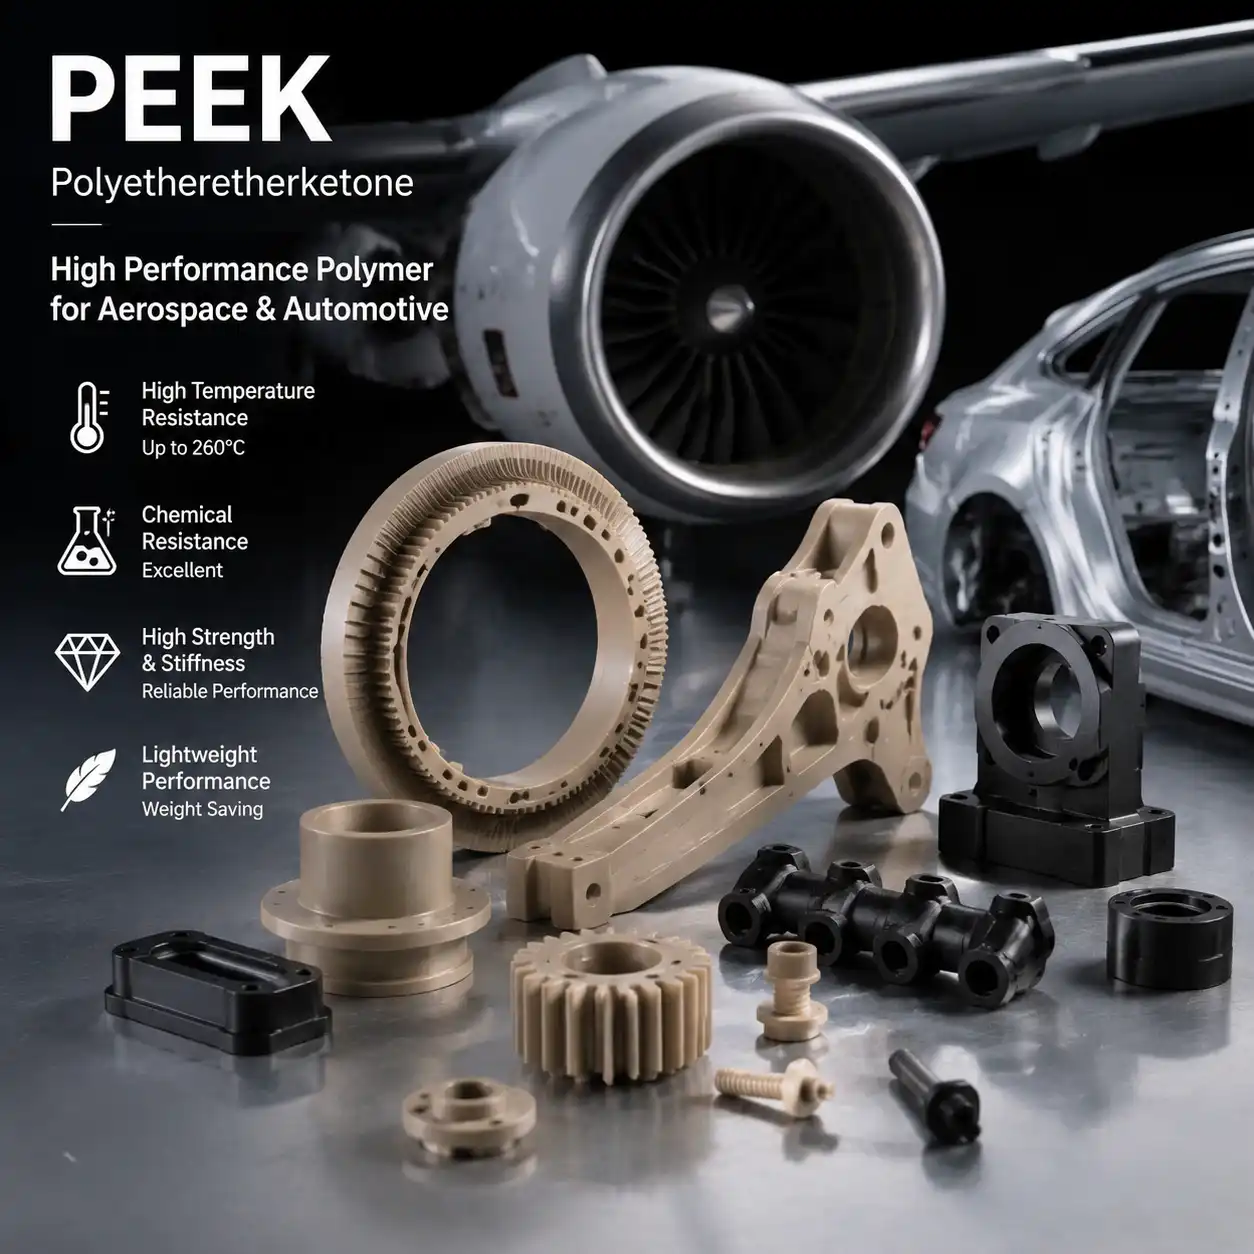
High-temperature polymers are less forgiving of moisture, residence time, venting and mold-temperature variation. Confirm the resin supplier’s drying window and transfer time. For injection molding, review mold temperature, fill speed, packing, cooling balance, gate location, weld lines and ejection. For CNC machining, confirm stock condition, tool wear, clamping force, heat generation, residual stress and the free-state condition during inspection.
- Keep wall thickness transitions gradual and use radii at internal corners.
- Place gates and weld lines away from the highest mechanical or sealing loads.
- Use the actual resin grade and reinforcement direction in flow and tolerance review.
- Define draft and ejection surfaces before approving texture or deep pockets.
- Separate cosmetic acceptance from functional acceptance at high-temperature surfaces.
- Measure critical features after conditioning or thermal exposure when fit depends on them.
How to prepare a high-temperature plastics RFQ
Send the CAD model, controlled drawing, resin or performance target, temperature profile, load case, chemical list, quantity, process preference, finish, color, critical dimensions and required documentation. State whether the part will be molded, machined or used as a prototype. Ask the supplier to identify the proposed grade, drying condition, tool or stock requirement, inspection method and any features that need a tolerance or material review.
For parts exposed to chemicals, provide concentration, temperature, exposure time, pressure, stress state and cleaning cycle. For electrical parts, include dielectric, flame, tracking or insulation requirements and the wall thickness at the critical location. For regulated applications, agree the exact grade and records before the purchase order rather than treating a polymer family name as approval evidence.
Qualification by process route
Injection molding is usually the preferred route for repeat quantities when the geometry, grade and annual demand justify a dedicated tool. The mold needs appropriate steel, heating, cooling, venting, ejection and surface treatment for the selected resin. A high-temperature material can produce acceptable plaques while still showing weld-line weakness, sink, flash or dimensional drift in the real part. Approve the mold with production-representative samples and inspect the critical features across the agreed cavity and process range.
CNC machining can be the better route for prototypes, low volumes, large sections or parts that need local precision without tooling. It introduces its own risks: stock may contain residual stress, thin walls may relax after clamping and the material can heat during cutting. Rough-machining, stress relief when appropriate, finish-machining and free-state inspection should be considered in the process plan. A hybrid route can machine sealing or bearing surfaces after molding when that is more economical than tightening the entire mold.
For procurement, compare suppliers on the complete route rather than resin availability alone: grade traceability, drying equipment, mold or stock capability, inspection records, pilot approval and change control all affect the delivered risk.
When the part is used near its thermal limit, qualify the complete assembly rather than the polymer alone. Check fasteners, inserts, seals, adhesives, lubricants and neighboring metals for different expansion rates or chemical response. Record the load applied during the thermal cycle and recheck fit, torque, leakage, insulation and movement after exposure. This converts a material choice into an evidence-based part approval.
Veelgestelde vragen
Welke hittebestendige kunststof is over het algemeen het beste?
Er bestaat geen universeel beste materiaal. PEEK biedt een brede combinatie van thermische, chemische en mechanische eigenschappen, terwijl PEI, PPS, PPA en LCP betere keuzes kunnen zijn wanneer elektrische eigenschappen, chemische stabiliteit, kosten, vloeibaarheid bij dunne wanden of maatvastheid de belangrijkste vereisten zijn.
Is PEI goedkoper dan PEEK?
PEI is vaak goedkoper in aanschaf en verwerking dan PEEK, maar de vergelijking hangt af van de kwaliteit, de hoeveelheid, de matrijzen, de bewerking, het drogen, de keuring en de kosten van defecten. Houd rekening met de vereiste gebruiksomstandigheden in plaats van alleen met de prijs van de kunststof.
Kunnen kunststoffen die tegen hoge temperaturen bestand zijn, worden gespoten?
Ja. PEEK, PEI, PPS, PPA en LCP worden in geschikte kwaliteiten spuitgegoten, maar voor elk materiaal gelden specifieke tijdvensters voor het drogen, smelten, vormen, ontluchten, afkoelen en uitwerpen. De matrijs en de machine moeten geschikt zijn voor het gekozen polymeer.
Welke informatie is nodig om een kunststof voor hoge temperaturen te kiezen?
Geef informatie over de continue en piekwaarden van temperatuur, belasting, blootstelling aan chemische stoffen, vochtigheid of stoom, elektrische of brandveiligheidsvereisten, geometrie, hoeveelheid, procesroute, toleranties en de vereiste inspectie- of nalevingsdocumentatie.
Hoe moeten de toleranties van kunststoffen bij hoge temperaturen worden gecontroleerd?
Gebruik gecontroleerde referentiepunten, een gedefinieerde toestand van het onderdeel en een methode die geschikt is voor het betreffende kenmerk. Controleer kritische onderdelen na het drogen, conditioneren of een representatieve thermische belasting en vergelijk het resultaat met de vereisten voor de samenvoeging.

