Injection molding draft angle is the release allowance that lets a molded surface move away from the cavity or core without dragging, scuffing or deforming the part. It should be selected from draw depth, resin shrinkage, surface texture, polish, stiffness, ejection direction and cosmetic requirements. A universal draft number is not reliable: a smooth shallow wall, a deep textured wall and a rib or boss can need different treatment in the same part.
For a buyer, the useful DFM review identifies the draw direction, marks surfaces that may show witness or drag, states the texture specification and explains any zero-draft or negative-draft condition. The supplier should show whether the proposed solution is added draft, a split line, lifter, slide, insert or a texture change, together with the dimensional, cosmetic, tooling and maintenance trade-off.
The engineering function of draft
| Draft decision | What it controls | Evidence to review | Risk when ignored |
|---|---|---|---|
| External wall draft | Release from the cavity and cosmetic wall movement | Draw direction, wall depth, texture and ejection direction | Drag marks, scuffing, sticking or dimensional distortion |
| Core-side draft | Part retention and release from the core | Shrinkage direction, polish, ribs, bosses and ejection force | Cracking, whitening, pin push or part retention |
| Texture allowance | Clearance for the textured surface to release | Texture depth, direction, draft map and witness limit | Texture drag, gloss change or torn surface |
| Rib and boss draft | Release of narrow internal features | Feature depth, thickness, radius and ejector support | Sticking, rib cracking, pin marks or broken features |
| Shutoff or lifter angle | Tool movement and sealing around an undercut | Slide/lifter travel, steel support and parting relationship | Flash, wear, mismatch or a tool concept that cannot open |
Review the mold design and mold making service page for the overall tooling path. The ejection design guide is useful when draft interacts with pins, sleeves, blades or stripper plates. The ribs and bosses guide covers internal features that often need their own release and support review.
Inputs that control the design
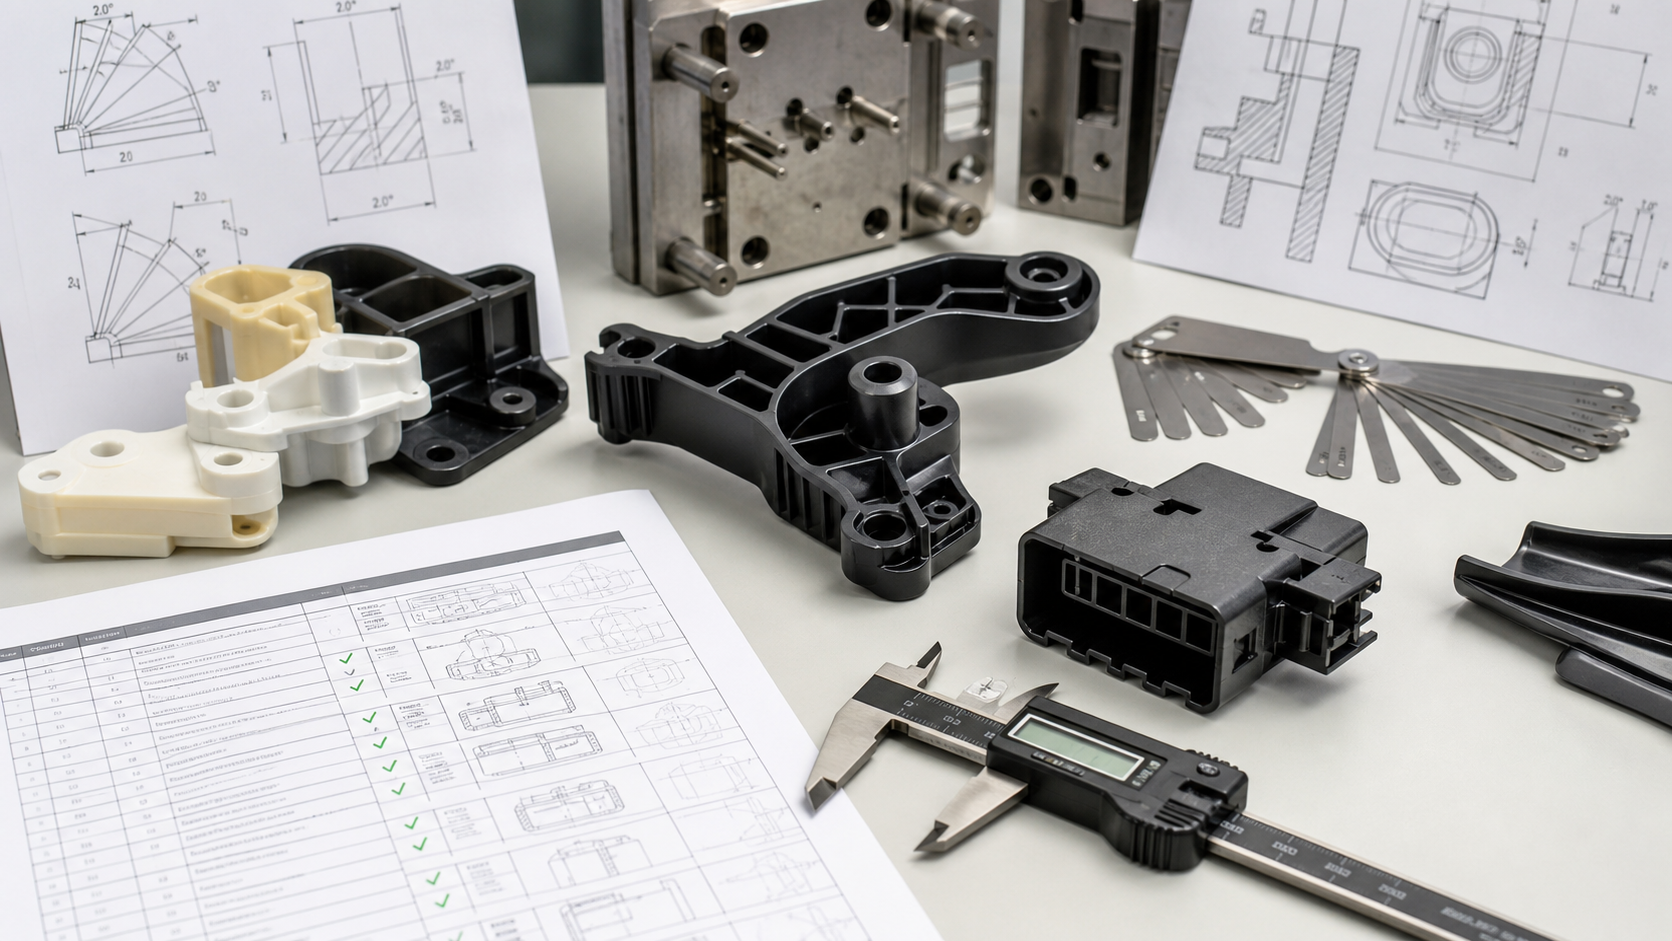
Draw depth is the first geometric input. A small draft over a shallow wall may release reliably, while the same angle over a deep wall can create significant surface drag. Shrinkage can make the part grip a core more strongly after cooling. The direction and amount of shrinkage vary with resin, filler, wall thickness, packing, mold temperature and flow orientation.
Surface finish changes the risk. A polished surface may release with less draft than a deep texture, but polish direction, scratches and vacuum can still cause drag. Textured surfaces need allowance for the texture depth and the direction in which the part moves. A cosmetic face should be reviewed with the texture supplier or toolmaker, not only with a nominal angle on the CAD model.
- Draw depth and the exact pull direction for each tool-moving surface.
- Resin grade, shrinkage, filler, stiffness and moisture condition.
- Surface finish, texture standard, texture depth and cosmetic viewing zone.
- Ribs, bosses, snaps, holes, shutoffs, inserts and undercuts.
- Ejector location, retention side, automation direction and gripper clearance.
- Critical dimensions, sealing surfaces, mating gaps and witness-mark limits.
Geometry rules for walls, ribs and bosses
Draft should be added in the direction of tool opening and should remain consistent with the functional geometry. When a wall must hold a dimension, the drawing should state whether the dimension is controlled at the shutoff, nominal plane, cosmetic face or assembly interface. Adding draft to a functional surface without revising the datum scheme can shift a mating feature even though the part releases more easily.
Ribs and bosses need draft on their sidewalls, sufficient radius at the base and enough support for ejection. A narrow deep rib with little draft may stick or whiten. A boss with poor core-side draft may retain the part and push a mark into the cosmetic face. If the feature is used for a screw, press-fit, seal or alignment, the release direction and tolerance must be reviewed together.
Shutoffs and slides are not substitutes for unlimited negative draft. A shutoff needs steel support, a workable angle, finishing access and a wear plan. A lifter or slide adds cost, motion, clearance and maintenance requirements. Sometimes the best solution is to move the parting line, split the insert, change the texture direction or redesign the feature so the tool opens with a simple draw.
Material and production-volume effects
| Material or condition | Draft concern | Design response | Trial evidence |
|---|---|---|---|
| Soft TPE or elastomer | Flexible walls can deform and grip texture during release | Increase release allowance, support the part and control ejection speed | Witness marks, ejection force, tear/whitening and automated removal |
| Glass-filled resin | Higher stiffness, shrinkage direction and tool wear can increase drag | Review core draft, polish, steel hardness and ejector support | Part retention, surface condition, dimensions and cavity comparison |
| Amorphous resin | Stress and surface finish can make drag visible even with modest shrinkage | Control polish, texture, temperature, packing and draw direction | Cosmetic boundary sample and stress/whitening inspection |
| Semi-crystalline resin | Shrinkage and crystallization can increase core retention after cooling | Review core draft, mold temperature, cooling and ejection timing | Free-state dimensions, ejection force and conditioned samples |
| High-volume tool | Wear, texture damage and changing release force accumulate | Define inspection, polish, texture and maintenance limits | Long-run witness trend, ejection stability and tool inspection |
Tooling options and cost trade-offs
Adding draft is usually the simplest tooling correction when the functional design allows it. It can reduce ejection force, simplify finishing and improve tool life. The cost may be a changed external profile, a revised texture boundary or a dimensional update that must be approved.
If draft cannot be added, the parting line can sometimes be moved to give each wall a usable draw. Slides and lifters can form undercuts, but they add motion, wear, clearance and maintenance. Inserts can isolate a difficult surface and make repair or texture replacement easier. A texture change can reduce drag when the appearance requirement permits it, but the texture supplier must confirm the actual depth and direction.
| Option | Voordeel | Trade-off | Suitable when |
|---|---|---|---|
| Add positive draft | Simple tool movement and lower ejection risk | May change profile, texture boundary or mating geometry | Functional surfaces allow a controlled angle |
| Move the parting line | Creates a simpler draw for separate surfaces | Moves witness line and may affect flash or cosmetics | Witness can be placed outside a critical zone |
| Use a lifter or slide | Forms an undercut or side feature | Higher tooling cost, motion, wear and maintenance | Undercut is essential to function |
| Use a replaceable insert | Localizes texture, repair or complex geometry | Insert fit, witness and alignment require control | High-value or repair-sensitive surface |
| Change texture or finish | Reduces release demand without changing core geometry | Appearance, gloss and customer approval may change | Cosmetic requirement permits an alternative texture |
Failure modes and corrective actions
Drag marks often follow the draw direction and may be visible only under angled light. Scuffing can come from insufficient draft, poor polish, texture direction, contamination, vacuum or excessive ejection speed. Stress whitening indicates local strain and should be evaluated with material, wall thickness, cooling and ejection force. Sticking may result from core retention, undercut, a hot section, inadequate draft or an ejector layout that pushes the part unevenly.
Do not assume more ejector force is the solution. Higher force can bend a wall, push a visible mark, crack a brittle feature or damage the tool. First identify the retention surface, verify mold temperature and cooling, inspect the core finish and confirm draft with a pull analysis or measurement. If the issue is limited to one cavity or one insert, investigate wear, polish, texture or alignment before changing the full mold.
Validation at DFM, mold trial and production approval
- Pull analysis: identify draw direction, negative faces, texture depth and the surfaces that need a draft decision.
- Tool review: check parting line, slides, lifters, inserts, ejector support, polish and finishing access.
- Trial witness: inspect drag, scuffing, whitening, pin push, sticking and texture damage as the mold opens.
- Force and speed: record ejection condition, cycle, mold temperature and automation repeatability.
- Dimensional check: measure critical profiles, holes, mating features and cosmetic surfaces after the defined conditioning state.
- Approval: retain an accepted boundary sample, draft map, witness limits and maintenance instruction.
DFM checklist and RFQ data package
- Provide 3D CAD, 2D drawing, resin, grade, texture and surface-finish requirement.
- Mark draw direction, cosmetic zones, critical dimensions, datums and allowed witness.
- State annual volume, tool-life target, automation direction and mold destination.
- Request a draft map covering walls, ribs, bosses, shutoffs, slides and lifters.
- Ask how ejection force, polish, texture and shrinkage will be validated.
- Define trial samples, boundary samples, inspection condition and acceptance limits.
For an RFQ, identify every surface that cannot move, show the preferred parting direction and state where witness marks are acceptable. We can then separate a true zero-draft requirement from a geometry that can use a small release allowance and avoid adding unnecessary slides or rework.
Draft Angle Decisions by Surface and Resin
| Surface Condition | Why Draft Changes | Review Before Tooling |
|---|---|---|
| Polished smooth wall | Lower friction may allow a smaller value, but shrinkage and depth still matter | Draw depth, steel finish, ejection force and cosmetic limit |
| Texture or grain | Texture increases mechanical lock and drag | Texture depth, draw direction, parting line and allowable scuff |
| Rib, boss or deep pocket | Thin features can flex, stick or mark during release | Feature thickness, core support, draft direction and pin access |
| Glass- or carbon-filled nylon | Shrinkage, stiffness, fiber orientation and surface behavior vary by grade | Exact PA grade, conditioning, flow direction, finish and trial evidence |
Draft should be agreed with the parting direction, texture, resin, cosmetic boundary, and ejection method. Adding a generic angle after the mold concept is fixed can move the parting line or create a new shutoff problem.
Hoe nylonplastic het project ondersteunt
Nylon Plastic has supported material selection and finished plastic-part manufacturing since 2005. For draft angle review for injection molded plastic parts, the useful review connects the drawing, material, tooling or machining route, inspection state, and production plan before a quote is approved.
- Review unfilled PA, PA-GF20, and PA-CF30 shrinkage, stiffness, texture, polish, and conditioning before approving a draft value.
- Connect draft to parting lines, slides, lifters, ejection, cosmetic samples, and the actual mold fabrication route.
- Mark critical cosmetic and sealing surfaces on the controlled drawing so draft changes do not create an unplanned fit or appearance issue.
Gerelateerde lezen
- Injection Mold Ejection Design
- Injection Mold Parting Line Design
- Op maat gegoten kunststofonderdelen
Veelgestelde vragen
What is draft angle in injection molding?
Draft angle is the taper that lets a molded surface move away from the core or cavity during opening and ejection without excessive drag, scuffing, or distortion.
Is there one standard injection molding draft angle?
No. The required value depends on draw depth, texture, polish, shrinkage, stiffness, resin, ejection support, and cosmetic requirements. A universal number can be misleading.
Does nylon need more draft than other plastics?
The answer depends on the exact nylon grade, shrinkage, texture, depth, stiffness, and ejection layout. Reinforced grades may change shrinkage and surface behavior, so validate the actual material.
What should be shown in a draft angle DFM review?
Show draw directions, parting line, texture, critical cosmetic and sealing surfaces, draft values, ribs and bosses, slides or lifters, ejection points, resin, and the sample acceptance standard.
Request an Injection Molding Draft Review
Send the CAD model, drawing, texture, resin, parting direction, and cosmetic requirements for a practical DFM review.

